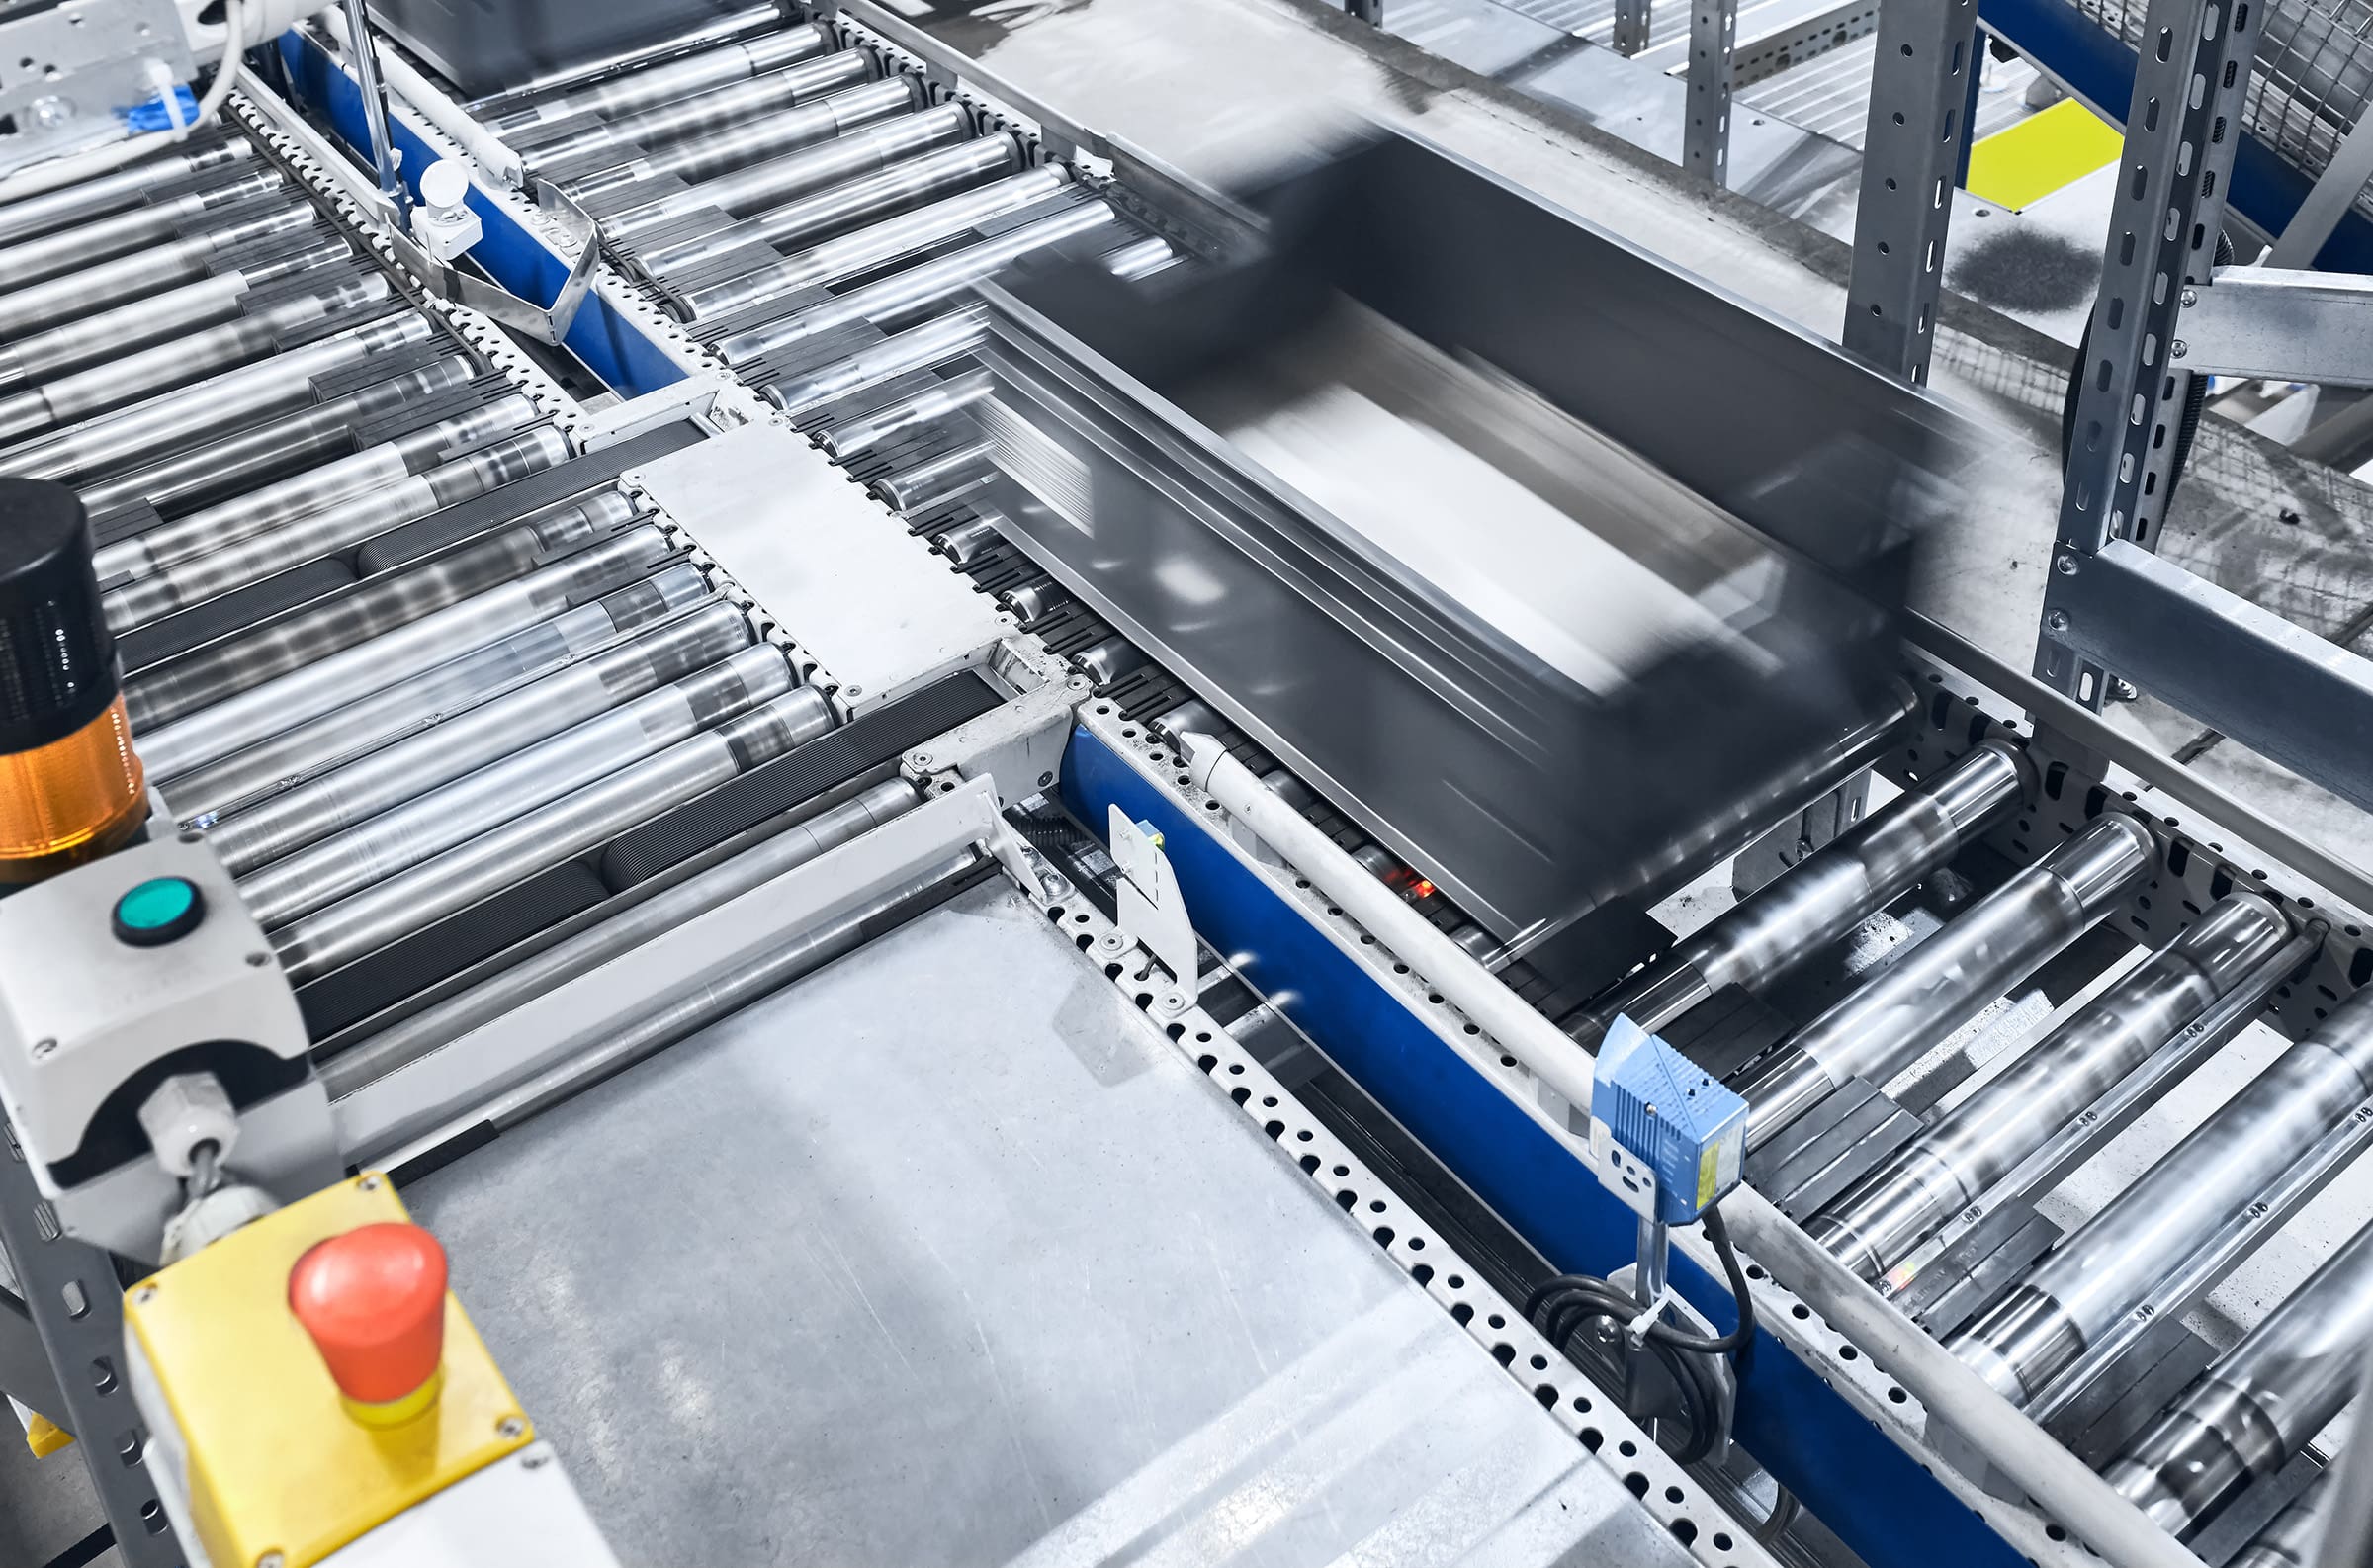
High-speed distribution centres and automated warehouses depend on extensive conveyor systems to move parcels and goods quickly. Choosing the optimal drive for these conveyors is key to achieving throughput targets and avoiding downtime. Warehouse conveyor drives must support rapid cycle times, with frequent merges and diversions. They must also run reliably around the clock and use energy efficiently. This guide explains how to select conveyor drives for high-speed warehousing. It covers speed and torque, space and maintenance in a busy logistics environment.
Industry & Application Challenges
Warehousing conveyors, especially in parcel hubs or fulfilment centres, face intensive duty cycles. They may run at high belt speeds to meet throughput targets. Sorters and merge conveyors also see constant stop-start action as packages are diverted. This puts wear on gearboxes due to frequent acceleration and braking. Load variability is another challenge. Some sections carry light parcels, while others see very heavy items. Drives must cope with this wide range.
There’s also a strong focus on energy efficiency – with hundreds of motors running, even small inefficiencies add up. Gearboxes need to be high-efficiency designs to minimise power consumption and heat generation. Space can be tight in dense conveyor layouts. Drive units often have to fit under low conveyor frames or between closely spaced lanes. Finally, many of these facilities run 24/7 with minimal downtime. Any gearmotor chosen should be highly reliable and quick to service or replace in the short windows available.
Choosing Warehouse Conveyor Drives
For high-speed conveyors, selecting helical or helical-bevel gearmotors is common because of their high efficiency and smooth operation. Sizing the gearbox and motor properly for peak loads is critical. A margin stops the motor running at full capacity all the time. This reduces wear and improves reliability. Variable frequency drives (VFDs) are a practical way to manage speed and soft-start conveyors. With a VFD-controlled motor, the gearbox accelerates belts gently, which reduces mechanical shock. The VFD can also adjust speed to traffic flow, saving energy when full speed is not needed.
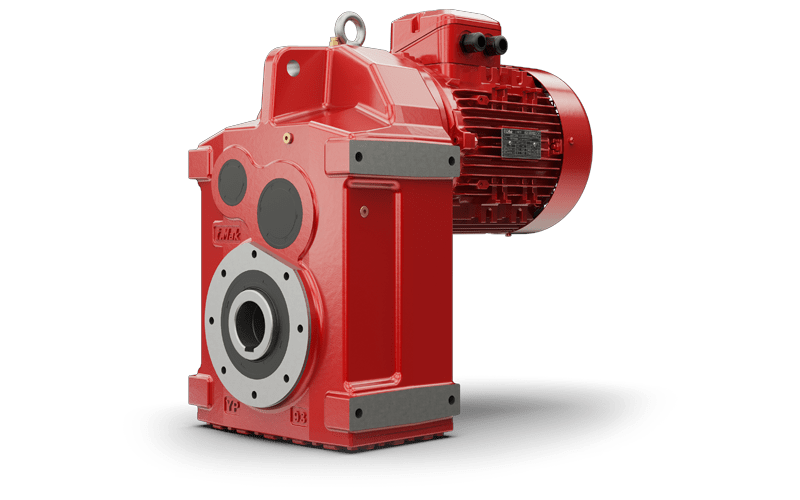
To address space issues, compact gearmotor designs are employed. I-MAK’s parallel shaft gearboxes (like the YP series) give a low-profile drive that fits under conveyors. Where vertical clearance is limited, right-angle gearboxes can tuck the motor to the side. These gearboxes can mount directly onto conveyor shafts with a torque arm, so no large base is needed. Their hollow output shafts also save space and simplify removal.
Reliability in high-speed systems often comes from small details. Examples include reinforced bearings for side loads such as belt tension, and synthetic oil for cooler running at high speed. Well-balanced moving parts also cut vibration at speed. Quick-change features are also valuable. For example, a motor flange lets you swap the motor without disturbing the gearbox mounting. A plug-in motor cable allows quick disconnection. Efficient design, correct sizing, compact fitting and easy maintenance all matter. Get them right, and warehouse conveyor drives keep throughput high with fewer unplanned stoppages.
Key Product Features
I-MAK IR Series gearboxes and YP Series parallel shaft gearboxes suit high-speed warehousing. Their key features include:
- High Efficiency & Power: Helical and helical bevel gearing runs efficiently, ensuring minimal energy loss even in 24/7 service. High torque output (up to ~18,000 Nm in the IR Series) provides ample power for heavy loads without sacrificing speed. This efficiency translates to lower running costs and cooler operation compared to outdated drive designs.
- Rugged, Continuous-Duty Design: These gearboxes have robust one-piece cast iron housings. They withstand shock loads and nonstop duty cycles. Heat dissipation and heavy-duty bearings suit continuous operation. That matters in busy distribution centres, where drives start and stop thousands of times a day.
- Flexible Configuration & Integration: A modular design with foot, flange or shaft mounting fits easily into most conveyor layouts. Wide ratio selections (from high-speed to high-torque ranges) mean you can optimise conveyor speeds without oversizing the motor. Units come ready to pair with IE3/IE4 motors and modern VFD controls for precise speed regulation.
- Integrated Safety & Feedback: Optional built-in backstops (holdbacks) are available to prevent roll-back on inclined conveyors, enhancing safety. Torque limiters can be fitted to protect against overloads. An oil temperature sensor is available as an option, which makes it simpler to add condition monitoring.
- Maintenance-Friendly Features: These conveyor drives are designed for minimal downtime. Hollow shaft and shaft-mounted models use a torque arm. You can remove and replace the gearbox by loosening a few bolts, which speeds up maintenance. Lubrication points and inspection covers are easy to reach. Clear oil change intervals, first after 500 hours and then every 6,000 hours, make service simple to plan. This focus on easy maintenance helps maximise uptime in high-throughput warehouse operations.
Illustrative warehouse conveyor selections
These scenarios show what to check, rather than claiming measured results from a warehouse project.
Parcel-hub drive replacement
When comparing existing worm drives with helical bevel geared motors, record torque, speed, starts, operating hours and the existing mounting. Compare efficiency at the actual operating points. Assess any on-demand control against throughput, restart torque and the rest of the line; do not assume that a new gearbox will automatically reduce energy use or downtime.
Mixed conveyor network
Choose the arrangement for each conveyor’s space and duty. A parallel shaft unit may suit one section, while a right-angle unit may fit a restricted transfer point. Synchronisation and positioning also depend on the motor, feedback and control system. Our VFD guide explains these control considerations.
Conclusion
Optimising conveyor drive selection is crucial for any high-speed warehousing operation aiming to maximise throughput, efficiency, and reliability. High-performance I-MAK IR Series and YP Series gearboxes keep warehouse conveyor drives running smoothly, with minimal energy waste or downtime.
Ready to elevate your conveyor performance? Explore our product pages for more details on the IR and YP series, or contact the Advanced Drives team for expert guidance in selecting the ideal drive solution for your facility. Our engineers are here to help you keep your warehouse moving at peak efficiency.